
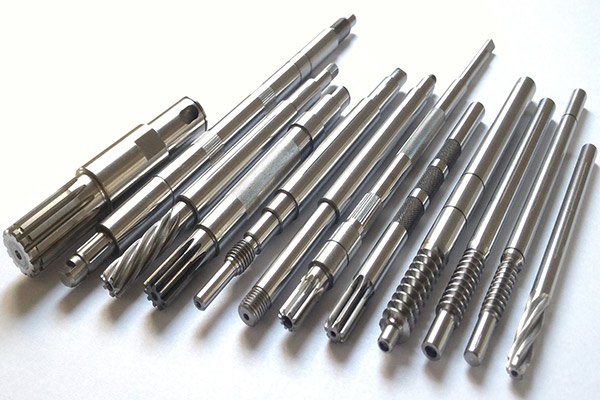
- Shaft
- Molds&Tools
- Hydraulics And Pump
- Hair transplant needle
- Hydraulics And Pump
- Precision CNC Shaft Machining Manufacturer for High Performance Applications
- Energy Industry CNC Machining Parts Supplier
- Aerospace Structural Components for OEM Programs
- Aerospace Structural Components for OEM Programs
- Automotive & EV CNC Machining Parts Supplier for OEM and Tier 1
- Medical Device CNC Machining Services
Integrating 3D Printing with Traditional CNC Machining for Rapid Prototyping

Integrating 3D Printing with Traditional CNC Machining for Rapid Prototyping
For global OEMs and Tier 1 suppliers, rapid prototyping is no longer defined by speed alone. A successful prototype must also represent the dimensional accuracy, material behavior, surface quality, assembly performance, and manufacturability of the eventual production part. Combining additive manufacturing with traditional CNC machining creates a practical bridge between early design validation and production-ready hardware.
1. Executive Summary
3D printing is highly effective for producing complex geometries, lightweight structures, ergonomic models, and early functional prototypes with minimal tooling. However, many printed parts cannot fully reproduce the tolerances, surface finishes, material properties, or interface accuracy required in industrial applications. CNC machining provides the precision and repeatability needed for critical datums, bearing seats, sealing surfaces, threaded features, and mating interfaces.
An integrated workflow uses each process where it delivers the greatest value. Additive manufacturing can create a near-net-shape blank or a geometrically complex prototype, while CNC machining finishes the surfaces and features that determine functional performance. This approach reduces development time, limits material waste, improves design feedback, and allows engineering teams to evaluate a part before committing to molds, dies, or dedicated production fixtures.
For procurement and supply chain leaders, the combined process also improves sourcing flexibility. A manufacturing partner capable of design support, additive prototyping, CNC production, inspection, and supplier coordination can shorten the transition from concept to qualified component. IndustryApex Technology, through IndustryApex CNC, supports this type of integrated precision manufacturing model for demanding industrial applications.
2. Technical Deep Dive
The most effective integration begins with a clear division of process responsibilities. 3D printing is generally selected for rapid geometry creation, internal channels, topology-optimized structures, and low-volume design iterations. CNC machining is then applied to establish functional datums, achieve tight tolerances, improve surface finish, and produce reliable interfaces with other components.
The first decision is whether the prototype should be printed in polymer, metal, or another engineered material. Polymer printing is useful for fit checks, ergonomic validation, airflow studies, cable routing, and assembly sequencing. It is fast and cost-effective, but it may not represent the stiffness, thermal expansion, wear resistance, or chemical compatibility of the final component. Metal additive manufacturing provides a closer approximation of production behavior, particularly for complex aerospace, medical, energy, and fluid-control parts, although it requires careful control of residual stress, porosity, support removal, and post-processing.
CNC machining adds value at several stages. A printed blank can be machined after stress relief to improve dimensional stability. Critical holes can be bored to a controlled position and diameter. Sealing faces can be milled or ground to meet flatness and roughness requirements. Threads can be machined instead of printed, ensuring stronger engagement and more consistent assembly torque. Reference surfaces can also be created so that inspection equipment and downstream assembly operations use repeatable datums.
Design for additive and subtractive manufacturing must be considered together. A wall may need additional stock for machining, while support structures should be positioned to minimize distortion on critical faces. Engineers should identify the surfaces that will remain printed and those that will be machined. This distinction affects orientation, allowance, clamping strategy, tool access, and inspection planning.
Digital manufacturing data is central to the workflow. A controlled CAD model should be linked to the printed build file, CNC program, revision history, inspection plan, and material documentation. Before machining, the supplier should verify stock condition, build orientation, reference features, and expected deformation. During machining, probing and in-process measurement can confirm that the part is correctly located before material is removed from high-value features.
Tolerance allocation is another important consideration. It is inefficient to apply production-level tolerances to every printed feature. Instead, the engineering team should classify dimensions according to function. Non-critical external contours may use additive tolerances, while bearing fits, sealing diameters, locating pins, and assembly interfaces receive CNC or grinding operations. This functional approach controls cost without compromising performance.
Surface finish requirements should also be mapped to process capability. Printed surfaces can contain stair stepping, partially fused powder, or directional texture. CNC milling can improve flat and accessible areas, while turning, precision grinding, EDM, or polishing may be required for specialized geometries. When the prototype is intended to predict production performance, the finished surfaces should match the expected production route as closely as practical.
Quality assurance must cover both processes. Typical controls include material certification, build records, heat treatment documentation, dimensional inspection, surface roughness measurement, leak testing, hardness verification, and first-article reporting. For safety-critical applications, computed tomography, dye penetrant, or other non-destructive testing may be appropriate. The final inspection plan should focus on the characteristics that influence function, not only on easily measured external dimensions.
In practice, the best workflow is iterative. A first printed model may validate overall form and assembly. A second version may combine additive geometry with machined interfaces. Subsequent prototypes can incorporate production-intent material, finishing, and inspection methods. This staged approach gives engineering teams useful evidence at each gate while avoiding premature investment in hard tooling.
3. The ODM & Supply Chain Advantage
The technical benefits of hybrid prototyping become more valuable when they are managed by a manufacturing partner with broader ownership of the supply chain. IndustryApex Technology’s core identity is that of a supply chain integrator and ODM solution provider. This means the engagement can extend beyond making a single prototype to include design-for-manufacturing feedback, process selection, material sourcing, secondary operations, inspection, packaging, and production transition.
For global OEM and Tier 1 suppliers, a controlled manufacturing system reduces communication gaps between engineering, purchasing, quality, and production. IndustryApex Technology operates a fully controlled precision manufacturing system supported by ERP and more than 30 years of manufacturing experience. Centralized production information improves revision control, purchasing visibility, capacity planning, and traceability across prototype and production orders.
The manufacturing edge includes 3-axis through 5-axis CNC machining, EDM, precision grinding, and industrial ceramics. This range of capabilities allows a prototype to move through multiple operations without requiring a new supplier for every specialized requirement. Five-axis machining can reduce setups and improve access to complex surfaces. EDM can produce narrow slots, sharp internal details, and difficult conductive materials. Precision grinding can establish tight dimensional relationships and superior surface finishes. Industrial ceramics provide options for applications requiring electrical insulation, wear resistance, thermal stability, or chemical durability.
A single integrated source can also improve technical decision-making. For example, a supplier that understands both CNC process limitations and additive design freedom can recommend whether a feature should be printed, machined, ground, or redesigned. It can identify where a printed structure needs machining allowance, where a nominal tolerance is unrealistic, or where a conventional process will provide better repeatability at production volume.
Supply chain resilience is another advantage. Prototype programs often fail to scale because the early supplier cannot support material certification, inspection documentation, capacity requirements, or repeatable process control. An ODM-oriented partner can plan the transition from prototype quantities to pilot production and recurring orders. This includes reviewing cycle time, fixture requirements, tool life, process capability, packaging, and logistics before the design is released for volume manufacturing.
ERP-supported coordination is especially important when multiple part numbers, revisions, and customer approvals are active at the same time. A controlled system can connect purchase orders, production status, inspection results, and shipment records. For OEM procurement teams, this improves forecast accuracy and helps identify risks before they affect assembly schedules.
The result is a more accountable development path. Instead of treating 3D printing as an isolated design activity and CNC machining as a later sourcing exercise, the two processes become part of one engineering and supply chain strategy. This reduces handoffs, improves manufacturability, and creates a clearer route to production qualification.
4. Industry Applications
Hybrid additive and CNC prototyping is relevant wherever complex geometry must be validated quickly but critical interfaces still require precision manufacturing.
Aerospace and Defense
Aerospace components often combine weight reduction, complex internal geometry, tight assembly interfaces, and strict documentation requirements. Printed structures can accelerate evaluation of lightweight brackets, ducting, tooling, and thermal-management components. CNC machining can then finish mounting surfaces, bores, threads, and aerodynamic interfaces. For production-intent work, specialized support for titanium and structural materials is essential. IndustryApex Technology provides dedicated expertise through its aerospace CNC machining and titanium aircraft parts capabilities.
Medical Devices
Medical equipment and implant-related development requires close attention to biocompatibility, dimensional control, surface condition, and traceability. Additive manufacturing can support anatomical models, custom device concepts, and complex low-volume geometries. CNC machining is well suited to final interfaces, surgical instrument features, precision bores, and titanium components requiring controlled finishes. Teams can review ISO-certified CNC machining for medical components when evaluating supplier capability.
Hydraulics and Fluid Control
Hydraulic manifolds, valve bodies, pump components, and fluid-control assemblies depend on accurate passages, sealing surfaces, threads, and intersecting bores. Printing can help engineers study routing and packaging, while CNC machining establishes the pressure-containing and sealing features needed for functional testing. Production documentation and leak testing should be defined early. IndustryApex Technology’s hydraulic pump parts manufacturing resources provide a relevant reference for these applications.
Industrial Automation and Machinery
Automation equipment frequently requires custom brackets, grippers, sensor mounts, end effectors, guide components, and replacement parts. Printed prototypes can validate motion envelopes and operator access before machining. Once the design is proven, CNC finishing can improve repeatability, wear resistance, and interchangeability across equipment platforms.
Energy, Semiconductor, and Specialized Equipment
Energy systems and semiconductor equipment often use parts with complex cooling channels, wear surfaces, high-purity requirements, or demanding thermal environments. A hybrid approach supports quick design iteration while preserving the precision needed for alignment, vacuum interfaces, fluid control, and component life. Industrial ceramics, EDM, grinding, and multi-axis machining can be combined when conventional printed materials are insufficient for final performance.
Across these sectors, the key performance measure is not simply how quickly a prototype is produced. The stronger measure is how effectively the prototype answers engineering questions about fit, function, reliability, manufacturability, cost, and production risk.
5. Call to Action
Integrating 3D printing with traditional CNC machining gives engineering and procurement teams a faster, more controlled path from concept to production. Additive manufacturing accelerates geometry development, while CNC machining delivers the precision, finish, and repeatability required for meaningful functional validation.
IndustryApex Technology and IndustryApex CNC can support global OEMs and Tier 1 suppliers with integrated ODM and supply chain services, including design-for-manufacturing review, 3-5 axis CNC machining, EDM, precision grinding, industrial ceramics, inspection, and production coordination. Visit the IndustryApex CNC home page to review manufacturing capabilities, or contact the engineering team with your CAD files, material requirements, target quantities, tolerances, and validation objectives.