
- Shaft
- Molds&Tools
- Hydraulics And Pump
- Hair transplant needle
- Hydraulics And Pump
- Precision CNC Shaft Machining Manufacturer for High Performance Applications
- Energy Industry CNC Machining Parts Supplier
- Aerospace Structural Components for OEM Programs
- Aerospace Structural Components for OEM Programs
- Automotive & EV CNC Machining Parts Supplier for OEM and Tier 1
- Medical Device CNC Machining Services
Batch Consistency in CNC Machining Buyer Guide: What OEM Teams Should Evaluate


When scaling from prototype to mass production, batch consistency in CNC machining determines whether your supplier can deliver 10,000 parts with the same dimensional accuracy, surface finish, and material properties as the first approved sample. OEM engineering and procurement teams must evaluate process control systems, statistical capability, and quality documentation to avoid costly rework, assembly failures, and field returns.
Key focus: This guide to batch consistency in CNC machining buyer guide explains the technical, quality, sourcing, and implementation criteria industrial buyers should validate.
Key answer: Batch consistency in CNC machining depends on machine thermal stability, tool-change protocols, material traceability, real-time SPC monitoring, and ERP-driven process control. OEM buyers should request Cpk data for critical dimensions, audit fixture and tool-management procedures, verify first-article and in-process inspection frequency, and confirm ISO-compliant documentation systems that link each part to machining parameters and inspection records.
Why Batch Consistency Matters in High-Volume CNC Production
In precision manufacturing systems, even minor variation compounds across thousands of parts. A 0.02 mm drift in a bearing seat diameter can cause assembly-line stoppages. Surface roughness variation affects seal integrity in hydraulic components. Material hardness inconsistency leads to premature wear in robotics gearboxes.
Batch consistency requires stable processes across shifts, tool changes, material lots, and machine maintenance cycles. Suppliers without formal process control rely on operator skill and post-inspection sorting, which increases scrap rates and hides systemic problems until production volumes rise.
Process Capability vs. Inspection Intensity
Process capability (Cpk) measures how consistently a manufacturing process stays within specification limits. A Cpk of 1.33 or higher indicates the process naturally produces parts within tolerance without excessive inspection. Suppliers with low capability compensate by inspecting every part or sorting batches, adding cost and time without addressing root causes.
Request Cpk studies for critical dimensions on similar parts. Verify that studies used production tooling, not prototype setups, and covered at least 25-30 consecutive parts across multiple tool changes. Suppliers who cannot provide recent capability data may lack the measurement systems or process stability required for high-volume CNC machining quality control.
Core Elements of Batch Consistency in CNC Machining
Machine Thermal Management
CNC machines expand and contract with temperature changes. A 5°C ambient shift can cause 0.01-0.03 mm dimensional drift on long parts. Consistent batch quality requires climate-controlled facilities, machine warm-up protocols, and thermal-compensation software that adjusts tool offsets in real time.
During audits, check for HVAC systems in machining areas, temperature logs, and whether machines run warm-up cycles before production starts. Suppliers operating in non-climate-controlled workshops struggle with morning-to-afternoon variation and seasonal drift.
Tool Management and Change-Over Protocols
Tool wear is the leading cause of batch drift. A worn end mill gradually increases hole diameter; a dull insert roughens surface finish. Effective tool management includes preset tool lengths, documented change intervals based on cut time or part count, and first-piece inspection after every tool change.
Ask how the supplier tracks tool life. ERP-integrated systems automatically flag tools approaching limits and require operator confirmation before resuming production. Manual logbooks and operator judgment introduce variability and missed changes.
Material Traceability and Lot Control
Material properties affect machinability and final part performance. Even certified stock varies slightly between lots in hardness, grain structure, and residual stress. Suppliers must trace each batch to material certificates, maintain lot segregation, and re-verify hardness when opening new stock.
Request the material traceability process. Systems that link part serial numbers to material lot, heat treatment batch, and machining date enable rapid root-cause analysis when field issues arise. Lack of traceability indicates weak quality control systems.
Statistical Process Control and Real-Time Monitoring
SPC tracks measurement trends to detect process drift before parts go out of tolerance. Operators measure critical dimensions at scheduled intervals, plot results on control charts, and trigger corrective action when trends approach limits.
Effective SPC requires calibrated measurement equipment, trained operators, and software that flags abnormal variation. During supplier evaluation, review control charts from recent production runs. Random patterns indicate stable processes; trends, jumps, or wide scatter reveal uncontrolled variation.
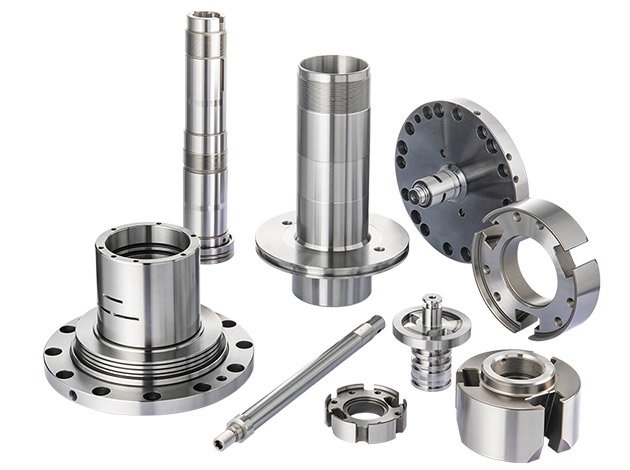
Batch Consistency Evaluation Framework for OEM Buyers
| Evaluation Criterion | What to Verify | Red Flags |
|---|---|---|
| Process Capability Data | Recent Cpk studies ≥1.33 for critical features, covering tool changes and multiple shifts | No capability data, studies from prototype runs only, Cpk below 1.0 |
| Inspection Protocols | Documented first-article, in-process frequency, final inspection; calibrated equipment with current certificates | 100% inspection as primary control, no calibration records, inspection after packaging |
| Tool Management System | ERP-tracked tool life, preset lengths, mandatory post-change inspection | Operator judgment for tool changes, no preset tools, missing change logs |
| Traceability | Part serial numbers linked to material lot, machine, operator, inspection data | No lot segregation, manual spreadsheets, certificates filed separately from parts |
| Corrective Action Process | Documented nonconformance reports, root-cause analysis, preventive measures, trend review | Verbal-only issue resolution, no failure tracking, repeated problems without corrective action |
Supplier Qualification Checklist
- Request process capability reports for features matching your critical dimensions and tolerances
- Verify climate control in machining areas and machine warm-up procedures
- Audit tool-management practices: preset tools, change intervals, post-change inspection records
- Confirm material traceability from certificates through finished parts, including heat treatment and secondary operations
- Review SPC control charts from recent production batches, checking for stable, centered processes
- Examine calibration certificates for measurement equipment used in process control and final inspection
- Request samples from three non-consecutive production batches and compare dimensional consistency
- Evaluate ERP or MES integration: real-time data capture, automated work instructions, nonconformance tracking
How ERP-Driven Manufacturing Improves Batch Consistency
Modern ERP systems for CNC mass production eliminate manual handoffs and operator interpretation. When a work order releases, the system pushes the correct program, tool list, inspection plan, and material specification directly to the machine and operator terminal. Process parameters, inspection results, and tool changes log automatically, creating a complete digital record for every part.
This integration prevents common batch-consistency failures: wrong program versions, skipped inspections, undocumented tool changes, and mixed material lots. Suppliers operating with paper travelers and manual data entry introduce transcription errors and rely on individual discipline rather than system enforcement.
Practical Steps for OEM Procurement Teams
Begin supplier evaluation with a detailed drawing review. Identify critical dimensions, surface finishes, and geometric tolerances that directly affect assembly and function. Request capability data specific to these features, not general machine accuracy specifications.
Conduct on-site audits focused on process control, not equipment lists. Observe actual production: Are operators following documented procedures? Are inspection intervals maintained during production pressure? Is nonconforming material segregated and tracked?
Require a pilot batch of 50-100 parts produced under normal production conditions, not prototype setups. Measure critical features across the batch and calculate capability indices. This trial reveals real process stability better than sample parts machined under special attention.
Establish clear quality agreements that define inspection frequency, documentation requirements, and corrective-action timelines. Specify measurement methods and acceptance criteria to avoid interpretation disputes. Include traceability requirements and data retention periods.
Frequently Asked Questions
What Cpk value should I require for critical CNC machined features?
For critical dimensions affecting fit, function, or safety, require Cpk ≥1.33, which ensures less than 64 defects per million opportunities when the process remains centered. For non-critical features with wider tolerances, Cpk ≥1.0 may suffice. Always request capability studies from production runs, not capability estimates based on machine specifications, which overstate real-world performance and ignore tool wear, setup variation, and material effects.
How can I verify a supplier’s batch consistency without a full production run?
Request historical control charts and capability studies from recent production of similar parts, focusing on comparable materials, tolerances, and feature types. Conduct a pilot batch of 50-100 parts machined consecutively under normal production conditions, measuring critical dimensions across the batch. Review inspection records and nonconformance reports from the past six months to identify recurring issues. Audit the tool-management system and observe actual tool-change procedures during a production shift.
What role does material traceability play in batch consistency?
Material traceability links each finished part to its raw material certificate, lot number, and heat treatment batch, enabling rapid root-cause analysis when dimensional or performance variation occurs. Different material lots exhibit slight differences in hardness, grain structure, and machinability that affect tool wear rates and final dimensions. Suppliers without lot control may mix stock, making it impossible to isolate whether variation stems from machining parameters or material properties.
Should I accept 100% inspection as evidence of quality control?
No. 100% inspection indicates the supplier lacks process control and must sort good parts from bad after machining. This approach increases cost, extends lead time, and does not prevent defects—it only catches them afterward. Effective quality control uses process capability, SPC, and preventive measures to produce consistent parts that require only sampling inspection. Rely on suppliers with documented Cpk ≥1.33 for critical features and risk-based inspection plans.
How do I evaluate a supplier’s corrective action process for batch inconsistencies?
Request recent nonconformance reports and review whether root-cause analysis identified process factors (tool wear, setup error, material variation) rather than blaming operator error. Verify that corrective actions included preventive measures such as revised tool-change intervals, improved fixtures, or enhanced process monitoring. Check whether similar problems recur, indicating ineffective corrective action. Effective suppliers track defect trends, conduct regular management reviews, and continuously update process control based on production data.
What documentation should I require to confirm batch consistency?
Require first-article inspection reports with full dimensional layout, in-process inspection records at defined intervals, final inspection reports, material certificates with traceability to part serial numbers, calibration certificates for measurement equipment, process capability studies for critical features, and SPC control charts from production batches. Documentation should link each part to machining parameters, tool usage, operator, and inspection results, enabling complete traceability and rapid issue resolution when variation occurs.
Conclusion
Evaluating batch consistency in CNC machining requires looking beyond machine lists and certifications to examine process control systems, measurement capability, and operational discipline. OEM teams should prioritize suppliers with documented process capability, ERP-integrated manufacturing, formal tool management, and material traceability that links every part to its production and inspection history. When you’re ready to qualify a supplier for high-volume production, upload your drawings along with critical dimension and batch-size requirements to receive a detailed capability assessment.
Sources
- JLCCNC, “Low Volume CNC Machining: Small Batch Production Guide,” https://jlccnc.com/blog/low-volume-cnc-machining
- TMCO, “CNC Machining Tolerances: What OEM Buyers Need to Specify,” https://www.tmcoinc.com/blog/high-precision-cnc-machining-how-modern-machine-shop-upgrades-improve-accuracy/